
“All-in-one” machine vision system for quality control on the production line, on automatic machines and on manual test benches. The new systems of the VISION CHECK 2000 series integrate a powerful machine vision system based on latest-generation image processing algorithms, a touch screen video interface and all the electronics required for interfacing with the production line or for remote control via fieldbus or standard I/O. The powerful functions made available by the control station allow both visual inspection operations and dimensional and geometric inspection operations to be carried out. The PCL2315 control station is equipped with a latest-generation industrial controller capable of processing the acquired images in real time, producing the inspection result within a few milliseconds. The ability to connect a very large number of cameras (up to 32 cameras), the ability to customise the lighting system and the complete configurability of the acquisition and processing software give the system very high flexibility, making it possible to address the full range of industrial inspection requirements with a single machine vision system.
 Vuoi un aiuto nella scelta del prodotto ?
Typical applications
- Vision systems for installation on production lines and automatic assembly machines.
- Vision inspection on robotic cells, on Cartesian manipulators or on manual test benches.
- ROBOT guidance in real time, automatic process control, feedback for the adjustment of automatic machines.
- Presence/absence inspection of parts on automatic assembly machines and verification of correct assembly.
- Dimensional and geometric inspection on the production line, verification in the metrology laboratory.
- Visual defect inspection and appearance inspection of the product.
Features
- “All-in-one” system integrating acquisition, processing, display and control in a single control station.
- Management of up to 8 cameras with smart cameras and PoE connection.
- Touch screen video interface that is intuitive and easy to use, designed for use even by untrained personnel.
- Possibility of connection to fieldbus (Profinet, EtherCAT, Modbus).
- Ethernet network connection for data exchange with management IT systems.
- Remote programming of production recipes and connection to external management databases.
Success stories

Dimensional inspection of electronic, electromechanical and mechanical parts.
Dimensional verification of diameters, thicknesses, widths and position of the components making up the assembled part. Verification of centre distances with automatic calculation of minimum, maximum and mean values. High-speed inspection even on non-oriented parts. Integrity or appearance inspection with colour discrimination and/or character recognition (OCR).

Reading of text and numbers with verification of the validity of the text string.
Reading of symbols, characters and logos with verification of character legibility or of correspondence with a reference master. Inspection of production and expiry dates with real-time verification of consistency with the production batch (OCR).

Inspection of integrity, position and orientation
Verification of the integrity of labels and electronic components with inspection of correct positioning and orientation. Integrity or appearance inspection with colour discrimination and/or character recognition (OCR). Verification of the absolute and relative position of components on PCBs and shape recognition.

Inspection of defects, presence of contaminants or dents.
Inspection of defects, bumps, dents, colour change, presence of contaminants and irregularities of shape. Real-time verification over the entire surface of the product, even with the product in motion or subject to vibration.

Inspection for surface defects or irregularities
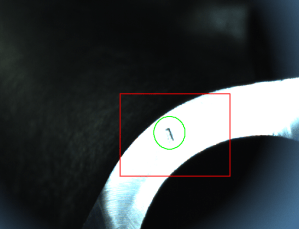
Verification of the presence of surface defects or irregularities on the surface, with identification of the distribution of the defects. Real-time calculation of defect size, of its distribution over the surface and of any abnormal concentrations of defects per unit area.

Dimensional and form inspection and comparison with the mathematical model
Dimensional and geometric inspection and comparison with the DXF mathematical model to determine non-conforming areas. Extraction of the dimensional features of interest and comparison with the reference mathematical model.

Identification of bulk objects and verification of orientation
Identification of the position and orientation of bulk objects or objects on conveyor belts, ROBOT guidance and control of Cartesian Pick & Place axes. Extraction of reference coordinates and angular coordinates for direct pick-up by ROBOT. Recognition system with artificial intelligence combined with machine vision.
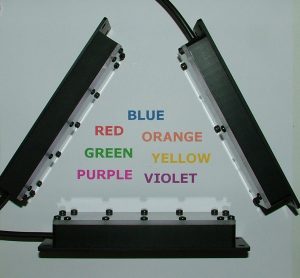
Colour inspection and discrimination
Colour discrimination and identification of the correct colouring of objects. Multichromatic lighting for the discrimination of particular product features or for colour discrimination determined by a change of contrast with the incident light. Wide choice of colours and wavelengths for comparative testing (red, green, yellow, blue, infrared, ultraviolet, white).

Profile inspection
Dimensional and geometric verification of the profile of mechanical parts. Extraction of the characteristic dimensions and comparison with a mathematical model or DXF drawing. Automatic calculation of widths, lengths, centre distances, thicknesses and diameters.

Verification of the position and presence of small parts
Inspection of small objects by means of microscopes or high-resolution magnification systems. Measuring systems based on high-resolution cameras, low-distortion optics or telecentric lenses. Micrometric inspection on precision mechanical components, electronic circuits and precision assemblies.

Verification of the presence of scratches or visual imperfections
Verification of the presence of scratches, marks, dents or visual imperfections that impair the appearance of the finished product. Inspection with matrix cameras or line-scan cameras. Real-time verification of defect size and of its distribution per unit area. Applications with backlight illuminators on wide continuous products.

Identification of the position and orientation of small parts
Identification of the position and orientation of small mechanical parts for use in automatic assembly systems. Selective inspection with determination of the pick-up coordinates for ROBOTs or automatic manipulators. Automatic inspection of orientation with optional rejection of parts that do not conform in shape and/or colour.
Strengths

The control station used in the systems of the VISION CHECK 2000 series is built to operate in industrial environments. It features design measures and construction techniques for a long operating life even in harsh environments or production situations with difficult ambient conditions.
15-inch monitor with industrial touch screen
Industrial monitor with touch screen control. High brightness and contrast. Suitable for industrial environments and for applications requiring high reliability and durability. The monitor is mounted on a support independent of the PC and can be replaced easily and quickly in the event of damage.
Fanless and diskless architecture
The use of the most modern heat dissipation techniques allows cooling fans to be eliminated (both on the CPU and inside the PC). All data and operating system storage media are based on FLASH SSD. The system is therefore also protected against vibration and mechanical stress.
LED beacon
Fault indicator with high-brightness LED beacon. As an option, the control station can also be fitted with an acoustic siren. The function of the beacon can be customised and can handle both warning and alarm conditions.
Tilting support
Mechanical tilting support for adjusting the inclination of the monitor and the controls (it can be installed on a table, on a pedestal or on a shelf). Option for connection to swing arms and overhead control pedestals.
Standard display and control interfaces
The system is based on an industrial embedded PC. Therefore, in the event of a temporary malfunction of the monitor or of the touch screen, a keyboard, a mouse or an office monitor can be used temporarily. This solution makes it possible to continue production even in the event of a temporary malfunction.
Intuitive software developed for machine operators
The software installed on board the VISION CHECK 2000 has been specifically developed for applications in industrial production. The main functions have been gathered into easy-to-read mimic displays with intuitive screens that can be handled even by non-expert personnel.
Front keypad
Front keypad for controlling the main system functions without touching the touch screen monitor (cycle start, cycle stop, fault reset, emergency). The operator can therefore work even while wearing gloves or in the presence of liquid contaminants. The front buttons can also accommodate an emergency button to be connected to the plant’s central control panel.
Removable SSD
Removable SSD for quick and easy commissioning in the event of modifications or malfunctions. The embedded PC has two separate SSD slots, allowing both periodic backups and duplication of the programs in use.
Integrated PLC
Integrated PLC for managing local I/O signals or for connection to existing production lines and electrical panels. Possibility of managing local control peripherals such as foot switches, remote keypads, light towers or audible signalling devices.
Industrial painted aluminium enclosure
Painted aluminium enclosure with security lock allowing access by authorised personnel only. The enclosure is fitted with gaskets that allow the control station to be used even in particularly dusty environments or in the presence of ambient contaminants.
Industry 4.0 connectivity and performance
Ethernet connectivity
The VISION CHECK 2000 control stations can be connected to any Ethernet network system for the exchange of production data, the sharing of test results, the programming of inspection recipes or of customised reports.

Connection to EtherCAT fieldbus
The systems of the VISION CHECK 2000 family can be connected to an EtherCAT fieldbus for data exchange and remote management of the synchronisation of the vision process.

Connection to MODBUS fieldbus
The systems of the VISION CHECK 2000 family can be connected to a MODBUS fieldbus for data exchange and remote management of the synchronisation of the vision process.

High-performance processors
The stations of the VISION CHECK 2000 series incorporate latest-generation processors of the Intel i5 and i7 families. The processors are programmed using the most modern multi-threading techniques available on the market.

PoE connection of the vision peripherals
All image acquisition peripherals (matrix and line-scan cameras, profile sensors and LASER scanners) are powered using Power over Ethernet or equivalent technologies. This minimises connection cabling and simplifies maintenance and operational changes.

Connection to PROFINET fieldbus
The systems of the VISION CHECK 2000 family can be connected to a PROFINET fieldbus for data exchange and remote management of the synchronisation of the vision process.

Remote assistance
The systems of the VISION CHECK 2000 family can be connected for remote assistance using Team Viewer technology. The RODER support team can ensure fast and prompt modification of the system’s operating conditions, even remotely.
Windows Embedded Technology
The control stations of the VISION CHECK 2000 series are based on the most modern processing technologies built on Windows Embedded.
Connection to management databases


The systems of the VISION CHECK 2000 series can be connected to the most widely used management databases. The connection to company databases allows the exchange of information regarding production batches, production times, reject rates and plant productivity indices.
High-performance cameras
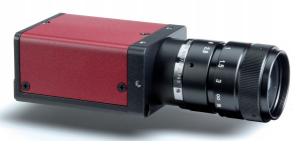
Matrix and line-scan cameras for any type of application, connectable to an Ethernet network with Power over Ethernet technology.
Resolutions up to 26 Mpx and the ability to handle up to 350 images per second.
Wide range of standard and telecentric lenses.
Accessories and customisation
A wide range of accessories completes the systems of the VISION CHECK 2000 series.
- LED illuminators for matrix cameras, in both backlight and front light mode.
- LED illuminators for line-scan cameras, in both backlight and front light mode
- Connection cables
- Optical filters and diffusers
Special customised systems

Do you need a turnkey system?
RODER is also able to propose and supply the complete system, with customised mechanics, electrical panels, pneumatic systems and all the assistance required for commissioning and personnel training.
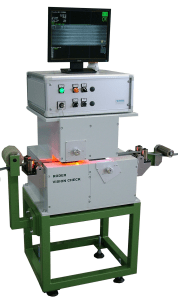
Vision systems with matrix and
line-scan cameras. Systems, sensors and software for image analysis with latest-generation
digital cameras. Versions with high-resolution monochrome or colour cameras
able to acquire and process the image within a few milliseconds.
A wide range of cameras, optics, filters, lighting systems, support mechanics and processing systems able to satisfy a wide range of applications and inspection requirements.
Integration into Industry 4.0 systems

Integrating machine vision systems into Industry 4.0 systems is an effective way of improving the quality of products and services. Machine vision systems are able to recognise objects, analyse images and respond quickly to changes in the environment. When used together with other technologies, such as artificial intelligence algorithms, production processes can become more efficient and more accurate. The result is better quality control and overall cost savings for companies.
Adding a machine vision system to an Industry 4.0 system can provide numerous benefits, both from the point of view of the human operator and from that of production. For example, a machine vision system can detect defects or imperfections in components that would go unnoticed by the human eye, leading to greater consistency in product quality. Furthermore, by automating certain aspects of product assembly, labour costs can be reduced while still ensuring the accuracy of production processes.

Machine vision systems also provide better safety measures when used as part of an Industry 4.0 system. Using image analysis and object recognition technology, a machine vision system is able to identify potential hazards that might otherwise go unnoticed by people on the factory floor. This helps reduce the risks associated with accidents or injuries caused by faulty machinery or unsafe working conditions.
Implementing a machine vision system within an Industry 4.0 system requires careful planning and execution in order to succeed. Companies must make sure that their existing infrastructure is compatible with the new technologies before attempting any integration process, and must also develop appropriate strategies for managing the data collected by these systems if they want to maximise their effectiveness in the operating environment. It is also important that systems of this kind are regularly tested and maintained to ensure that they continue to deliver accurate results over long periods of time.

Integrating machine vision systems into Industry 4.0 systems has the potential to revolutionise production processes in many ways, from data collection and analysis through to the prevention of defective products.
With the help of advanced machine vision algorithms, companies can detect objects, measure dimensions and inspect surface defects with unprecedented accuracy. By automating inspection and quality control, companies are also able to reduce the costs associated with manual work and increase overall productivity.
When integrated into an Industry 4.0 system, machine vision technology can enable more efficient access to real-time data and analytics. This means that companies can quickly assess the condition of their products and identify areas for improvement from any location. Moreover, automated inspection not only improves accuracy but also helps prevent the errors that can arise from overloading staff or from human error in making quality control decisions.
To ensure that business operations run smoothly, companies must make sure that their machine vision systems are successfully integrated into their Industry 4.0 framework.
The system must be built using an architecture that delivers high quality. The system must be built using an architecture capable of accommodating all the necessary input devices, such as cameras and sensors, while ensuring sufficient scalability for future upgrades or expansion. It is also important that manufacturers choose components and algorithms suited to the specific application they have in mind, since these will determine the accuracy of the inspection results.
Machine vision systems offer numerous benefits when used within Industry 4.0, including greater accuracy in product inspection, a reduction in the labour costs associated with manual inspection, and better access to real-time data analytics to improve decision-making.

Companies must make sure that their system is built correctly so as to derive the greatest benefit from this technology, and must choose components carefully so that they perform optimally for their specific needs. By integrating machine vision technology into their existing infrastructure, companies can benefit from greater efficiency at lower cost, while also improving safety conditions for the workers involved in quality control processes, who no longer have to carry out hazardous work manually thanks to the automation these systems make possible.
You must be logged in to post a comment.