






RODER · Inspection · Dimensions and geometry
Automatic dimensional measuring systems
Automatic dimensional measurement and vision systems represent the technological evolution of industrial metrology, integrating precision sensors, handling systems and dedicated software for the geometrical inspection of components and products in the laboratory and directly on the production line. They comprise contact solutions such as coordinate measuring machines, systems with inductive LVDT probes, multi-gauge stations, machine vision systems and robotised cells dedicated to quality control on large volumes.
On this page
What the measurement is for: automatic dimensional measuring systems ↑ up
Automatic dimensional measurement systems are used in the automotive and aerospace sectors for the inspection of critical components such as engine blocks, turbine blades, body shells and gears, in rapid prototyping laboratories for reverse engineering, in statistical quality control (SPC) of series production, in the inspection of electronic assemblies for verifying placement and coplanarity, and on drawing and rolling lines for continuous dimensional measurement. Being able to integrate measurement into the production cycle drastically reduces inspection times and the number of non-conforming parts.
Operating principles ↑ up
Coordinate measuring machines (CMM) acquire points by means of piezoelectric contact probes or optical probes, reconstructing the geometry of the workpiece in Cartesian space with resolutions below the micrometre. Machine vision systems use high-resolution cameras, dedicated illuminators and image-processing algorithms (edge detection, sub-pixel) to extract geometrical measurements from two-dimensional images. LVDT probes (Linear Variable Differential Transformer) exploit inductive coupling to measure displacements with nanometre resolution. Laser triangulation and time-of-flight systems allow non-contact measurement of profiles and flatness.
Types of systems covered ↑ up
This section brings together manual, motorised and DCC coordinate measuring machines, machine vision systems for dimensional inspection and surface inspection, multi-gauge units with LVDT and inductive probes, laser systems for flatness and multiple-geometry measurement, high-speed cameras with their accessories (telecentric lenses, structured lighting), and robotised cells for measurement automation with the integration of articulated arms and industrial fieldbuses.
Regulations and standards ↑ up
The acceptance and periodic verification of CMMs are governed by ISO 10360 in all its parts (probing error, length error, scanning error, performance with articulating probe heads). Geometrical product specifications follow the GPS system (Geometrical Product Specifications) ISO 1101 and, in the American context, ASME Y14.5 for GD&T. The declaration of conformity of measurements complies with ISO 14253-1, while reference standards (rings, spheres, gauge blocks, ball bars) must be calibrated in accordance with ISO 17025.
Integration and Industry 4.0 ↑ up
Modern automatic systems offer digital interfaces (Profinet, EtherCAT, OPC UA, MQTT) for integration with company SCADA, MES and ERP systems. The measurement data is archived, analysed statistically and correlated with process parameters, enabling adaptive production control strategies. The child pages of this hub present each category in detail, with further information on metrological performance, hardware configurations and selection criteria according to the application.
The selection of a measuring system must take into account the trade-off between precision, speed, complexity of integration and life-cycle cost. A correctly sized system not only reduces scrap and increases productivity, but also generates process data that feeds company analytics systems and enables predictive maintenance strategies. The technological choice should always be validated by a feasibility study on the real sample, including MSA (Measurement System Analysis), Gage R&R and calculation of the expanded uncertainty in accordance with the GUM.
The pages in this section ↑ up
The in-depth pages for this quantity: techniques, selection criteria and instrument families.
In depth
Coordinate measuring machines (CMM)
→
Manual, motorised and DCC CMMs with contact and optical probes for complete geometric measurement.
→
Multi-gauge dimensional and geometric inspection stations (modulcheck, digicheck) with industrial displays.
→
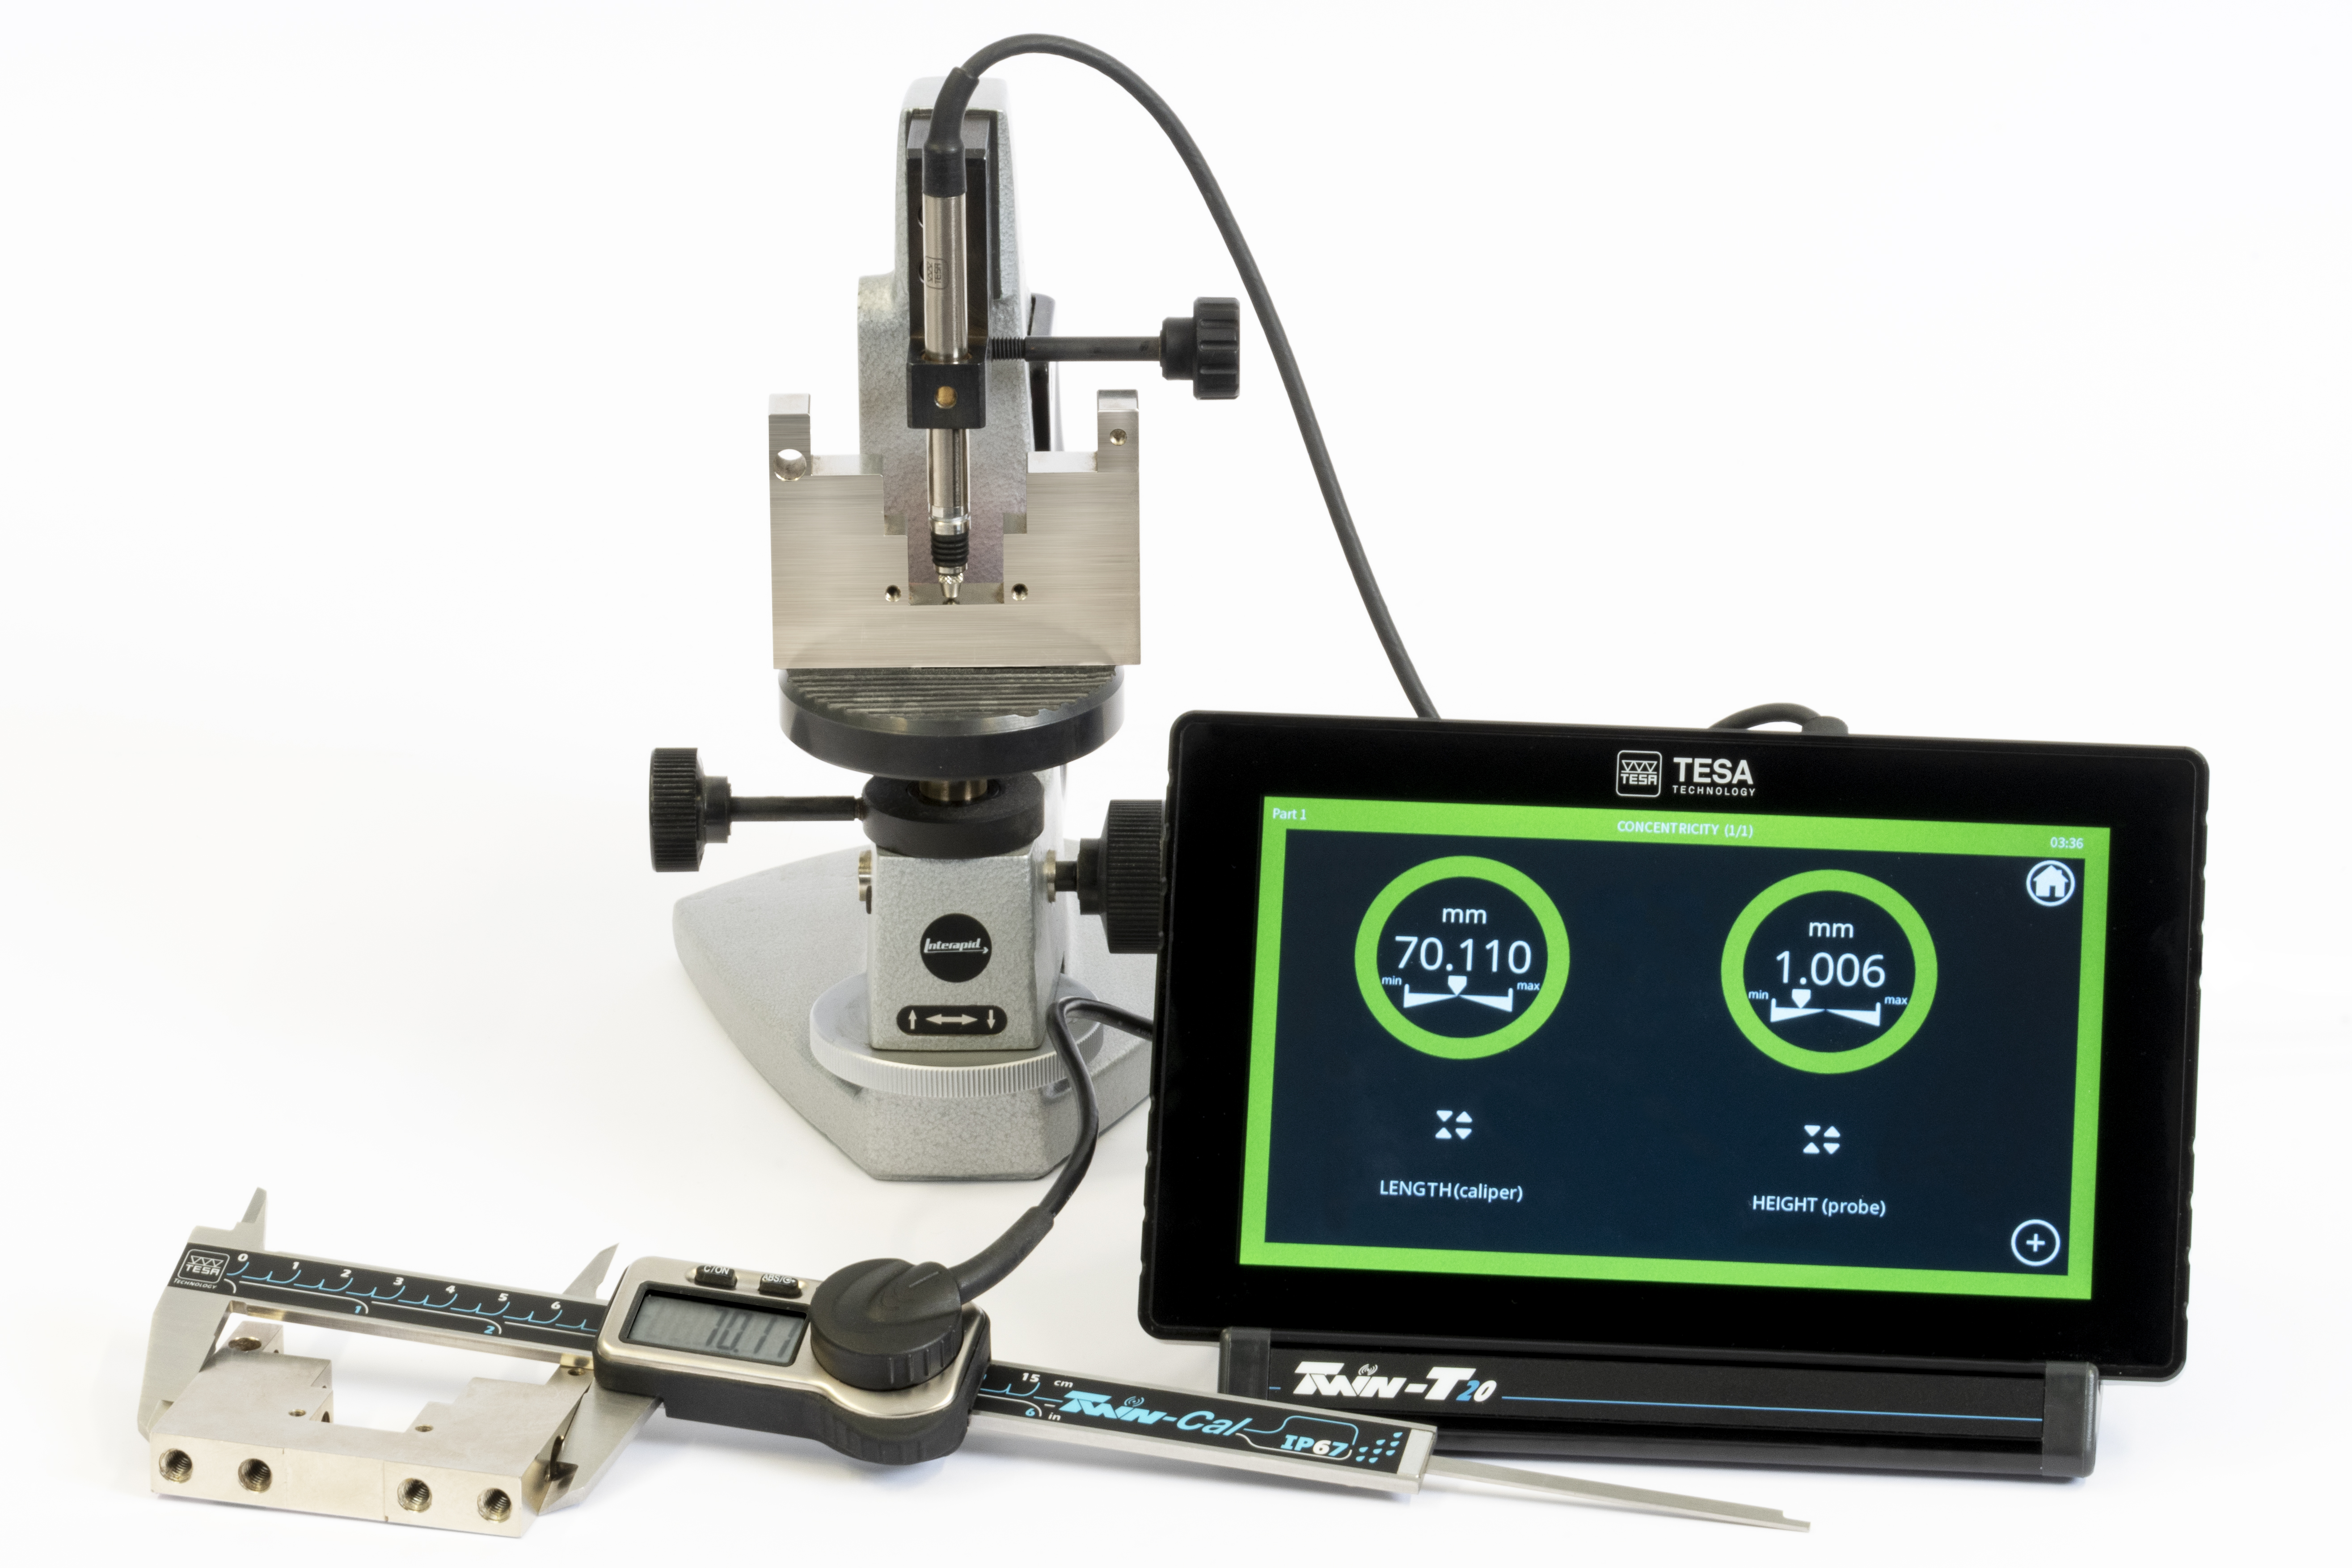
LVDT linear transducers, inductive gauges and digital displays for precision measurement.
→

Automated dimensional and geometric measuring systems with robot and fieldbus integration.

Laser systems for flatness inspection, positioning and geometric measurement on the production line.
Vision division · VISIOTRONIX
The right lighting for this inspection is on visiotronix.com
Photolux LED bars, ring lights, backlights, flat domes and spotlights, with technical guidance for choosing the geometry and quality of light according to the defect or dimension to be inspected. Complete vision systems remain in the RODER Systems catalog.
The information on this page is provided for information purposes. Although it has been compiled with the greatest care, it may contain transcription errors or typos: for precise, up-to-date information please contact RODER SRL directly.
Contacts & Information
Contact for general information : info@roder.it
Machine Vision Division of RODER : www.visiotronix.com
RODER Instruments Division : www.innovacheck.com
More about RODER : about us
The information contained in this website is provided for information purposes only. Although it has been prepared with the greatest care, it does not constitute a contractual offer or a binding commitment to supply. It may contain transcription, translation or typographical errors. For precise and up-to-date information, please contact our company directly.
Note: Some images on this website have been intentionally generated using artificial intelligence (AI). This is because, for many applications and projects, photographs of the actual installation or system cannot be disclosed owing to confidentiality agreements, contractual clauses and non-disclosure agreements (NDAs).
You must be logged in to post a comment.