





RODER · Inspection · Dimensions and geometry
Distance and position
Non-contact measurement of distance, position and displacement is a key technology for industrial applications in which the speed of the process, the fragility of the material or the inaccessibility of the measuring point make traditional methods unsuitable. Laser, capacitive, inductive and optical sensors make it possible to acquire thousands of measurements per second on moving surfaces, hot materials, products being processed or delicate objects, eliminating mechanical wear and contact errors.
On this page
What the measurement is for: distance and position ↑ up
Non-contact sensors are used in the continuous measurement of products in extrusion, rolling, drawing and calendering, in position control of robots and actuators in industrial robotics, in level checking in tanks and hoppers, in the positioning of cranes and industrial trucks, in the predictive maintenance of rotating machines for run-out measurement, and in the detection of point defects on continuous webs (laminates, plastic films, non-woven fabrics). Integrating several sensors allows the three-dimensional reconstruction of complex profiles.
Non-contact measuring principles ↑ up
The most widespread techniques are: laser triangulation, in which a collimated beam is projected onto the target and the reflected image is acquired by a CMOS/CCD sensor positioned at an angle, the distance being derived from the position of the spot on the array; time-of-flight (ToF), which measures the flight time of a light pulse modulated in phase or in amplitude; laser interferometry for very high resolution measurements; chromatic confocal sensors, which use chromatic dispersion to measure the distance and the thickness of transparent materials; and capacitive and inductive sensors for short-range applications in an industrial environment.
Instrument types ↑ up
The section comprises portable laser distance meters for quick measurements on site and in industry, industrial laser distance sensors (triangulation and ToF) for integration into machines and plants, high-resolution position and displacement sensors (capacitive, inductive, eddy current) for precision applications, specialised detectors of holes and discontinuities on moving webs (punch hole detection), and laser lines and levels for alignment and marking out. Each family covers different ranges, resolutions and accuracy classes, according to the sector of use.
Laser safety and regulations ↑ up
The use of laser sources is governed by IEC 60825-1, which defines the safety classes (1, 1M, 2, 2M, 3R, 3B, 4) and the protective measures required. Industrial sensors belong predominantly to classes 1 and 2, which are inherently safe. For CE marking and use in classified environments, EN 60204-1 (electrical safety of machinery) applies and, for explosive atmospheres, the ATEX Directive 2014/34/EU. Sensor specifications also follow VDI/VDE 2634 for optical measurement of form and dimension.
Selection criteria ↑ up
Choosing the right sensor depends on the measuring range, the resolution required, the acquisition bandwidth (Hz/kHz), the characteristics of the surface to be measured (reflectivity, roughness, colour, geometry), the operating environment (temperature, dust, vibration), the output interface (analog, digital, fieldbus) and the safety requirements. In the child pages each technology is examined in more detail, with typical parameters and application guidance.
The selection of a measuring system must take into account the trade-off between precision, speed, complexity of integration and life-cycle cost. A correctly sized system not only reduces scrap and increases productivity, but also generates process data that feeds company analytics systems and enables predictive maintenance strategies. The technological choice should always be validated by a feasibility study on the real sample, including MSA (Measurement System Analysis), Gage R&R and calculation of the expanded uncertainty in accordance with the GUM.
The pages in this section ↑ up
The in-depth pages for this quantity: techniques, selection criteria and instrument families.
In depth
Handheld laser distance meters
→
Handheld laser distance meters for industrial and construction use, with ranges from a few meters to hundreds of meters.
Laser triangulation sensors for measuring distance, displacement and position in production.
Transducers for measuring displacement, low-frequency vibration and high-precision positioning.
In depth
Non-contact distance measurement
→
Non-contact distance measurement with LASER distance meters makes it possible to detect distances, positions and levels quickly and accurately, even on moving objects…
Sensors for detecting holes, slots and discontinuities on webs moving at high speed.
In depth: in-line non-contact measurement ↑ up

In-line non-contact measurement of speed and length monitors the material as it runs, in real time, eliminating the wear and slippage typical of contact systems.
- In-line measurement: in real time
- Non-contact: no wear or slippage
- High speed: up to 50 m/s
- High accuracy: uncertainty down to 0.025 %
- Wide range of materials: metal, paper, wood, plastic
- Standard outputs: encoder, analog and bus
- Easy integration: direct process control
In-line non-contact measurement of speed and length is one of the most requested solutions in process automation: it makes it possible to monitor the material as it runs, without touching it, eliminating wear and slippage. ASTech optical velocimeters and encoders perform this measurement in real time, with constant accuracy and repeatability.
This page belongs to the Automation and industrial process section and describes how to measure speed and length directly on the production line.
What in-line non-contact measurement means
Measuring in-line means detecting the quantity of interest while the material is in production, without interrupting the process. Doing so without contact adds a decisive advantage: since there are no parts touching the material, there is no wear, slippage or marking of the surface. The optical velocimeter illuminates the material with LED light and analyses the reflected light, deriving the instantaneous speed and, by integration, the length. As a result, the measurement remains accurate and repeatable over time, even on hot, thin, glossy or delicate materials.
For fast lines the VLM500 is used (up to 50 m/s, uncertainty < 0.025 %); for low speeds and the replacement of measuring wheels the VLM60, accurate even at 0 m/s.
Functions enabled by in-line measurement
In-line measurement feeds numerous automation functions: cut-to-length, piece counting, synchronisation between drives, elongation control and production documentation. For example, knowing the actual speed of the material makes it possible to trigger a shear at the exact instant, or to keep the ratio between two motorised rollers constant. In other words, in-line measurement turns raw data into concrete control actions.
Advantages of in-line measurement
- Monitoring of the material in production, without stopping the process
- No wear or slippage: data stable over time
- Suitable for hot, thin, glossy or delicate materials
- Fast update time for real-time control
- Integration with PLCs, drives and supervision systems
Real time and signal dynamics
In process control, not only accuracy counts but also the responsiveness of the data. The optical velocimeter updates the measurement in less than a millisecond and offers a configurable moving average, useful for stabilising the signal without losing reactivity. These high dynamics make it possible to follow rapid transients, such as line start-ups or load variations, while also keeping the length measurement by integration accurate. As a result, the control loops work in a more stable and precise way.
In addition, the availability of the data on encoder, analogue and fieldbus outputs makes it possible to feed several systems at the same time, from cutting control to line supervision.
Robustness and installation
In-line measurement requires robust instruments, capable of working continuously in industrial environments. With IP 65 protection, white-light LED illumination and, where necessary, protective housings, ASTech optical velocimeters offer high availability with minimal maintenance. Installation is facilitated by plates and alignment units, which ensure correct positioning with respect to the material. Ultimately, in-line non-contact measurement improves the quality and continuity of the process, with a rapid return on investment.
Recommended products

VLM500 optical speed meters
Speeds up to 50 m/s, uncertainty < 0.025 %, CCD spatial filter.

VLM60 optical encoder
A replacement for measuring wheels, measuring down to 0 m/s.

Optical encoder speed meters
Overview of the optical speed meter and encoder family.
Measurable quantities and available signals
In-line measurement provides two fundamental quantities: the instantaneous speed of the material and its length, obtained by integration. These data are made available on A/B incremental encoder outputs, an analogue current output and the main fieldbuses. In this way the same instrument feeds both the fast control loops, via the encoder output, and the supervision systems, via the fieldbus. As a result, integration is flexible and suited to different automation architectures.
Comparison with contact measurement
Compared with measuring wheels, in-line optical measurement eliminates slippage and wear at the root, the two main sources of error and maintenance. Wheels, moreover, can mark delicate materials and have to be replaced periodically; the optical velocimeter, on the other hand, does not touch the material and keeps accuracy constant over time. In practice, optical measurement offers higher data quality at a lower running cost.
Maintenance and availability
In an automated plant, every unplanned stoppage has a high cost. The absence of contacting parts reduces maintenance to minimal interventions, such as periodic cleaning of the optical window. With IP 65 protection and, where needed, protective housings, the instrument guarantees high availability even in continuous operation. Ultimately, in-line non-contact measurement contributes to a more stable, documented and productive process.
An investment that pays for itself
In-line non-contact measurement combines accuracy, responsiveness and reliability, reducing scrap and unplanned stoppages. On continuous, high-volume processes, these benefits quickly translate into a tangible return on investment. In addition, the possibility of directly replacing measuring wheels and rotary encoders, replicating their signal, makes adoption simple and low-risk. RODER technical support helps to assess the application and define the most suitable solution, from the choice of model to the installation accessories. It should also be considered that reliable and documented process data is today an increasingly requested requirement in view of digitalisation and connected industry, where the quality of in-line measurements is the prerequisite for any subsequent analysis and optimisation.
Frequently asked questions
What is in-line non-contact measurement?
It is the measurement of the speed and length of the material while it is in production, carried out optically without touching it, and therefore without wear or slippage.
Which automation functions does it enable?
Cut-to-length, piece counting, drive synchronisation, elongation control and production documentation.
Is the signal suitable for real-time control?
Yes. The update time of less than a millisecond makes the data suitable for fast control loops.
Does it work on hot or delicate materials?
Yes. Non-contact measurement, with the appropriate housings, remains valid on hot, thin, glossy or delicate materials.
How is it integrated into the plant?
Through incremental encoder, analogue and fieldbus outputs, compatible with existing PLCs, drives and supervision systems.
Related products
The RODER instruments for this application. Go to the relevant catalogue pages for models, technical data and documentation.
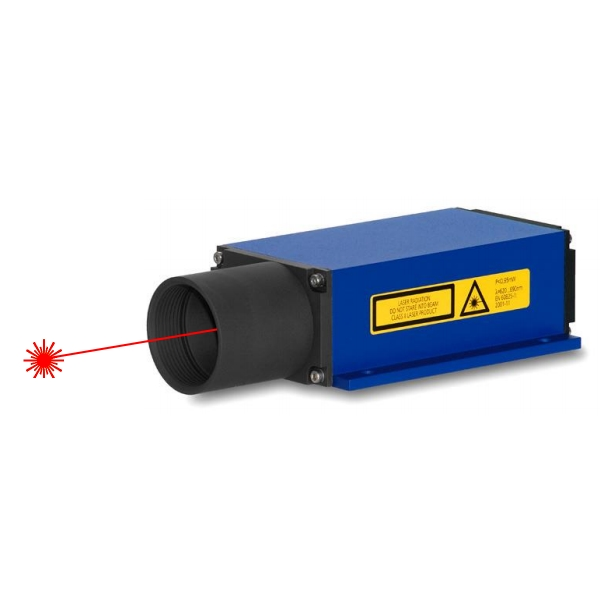
Industrial LASER distance sensors
LDM LASER distance sensors for non-contact distance, position and level measurement.

Vision division · VISIOTRONIX
The right lighting for this inspection is on visiotronix.com
Photolux LED bars, ring lights, backlights, flat domes and spotlights, with technical guidance for choosing the geometry and quality of light according to the defect or dimension to be inspected. Complete vision systems remain in the RODER Systems catalog.
The information on this page is provided for information purposes. Although it has been compiled with the greatest care, it may contain transcription errors or typos: for precise, up-to-date information please contact RODER SRL directly.
Contacts & Information
Contact for general information : info@roder.it
Machine Vision Division of RODER : www.visiotronix.com
RODER Instruments Division : www.innovacheck.com
More about RODER : about us
The information contained in this website is provided for information purposes only. Although it has been prepared with the greatest care, it does not constitute a contractual offer or a binding commitment to supply. It may contain transcription, translation or typographical errors. For precise and up-to-date information, please contact our company directly.
Note: Some images on this website have been intentionally generated using artificial intelligence (AI). This is because, for many applications and projects, photographs of the actual installation or system cannot be disclosed owing to confidentiality agreements, contractual clauses and non-disclosure agreements (NDAs).
You must be logged in to post a comment.